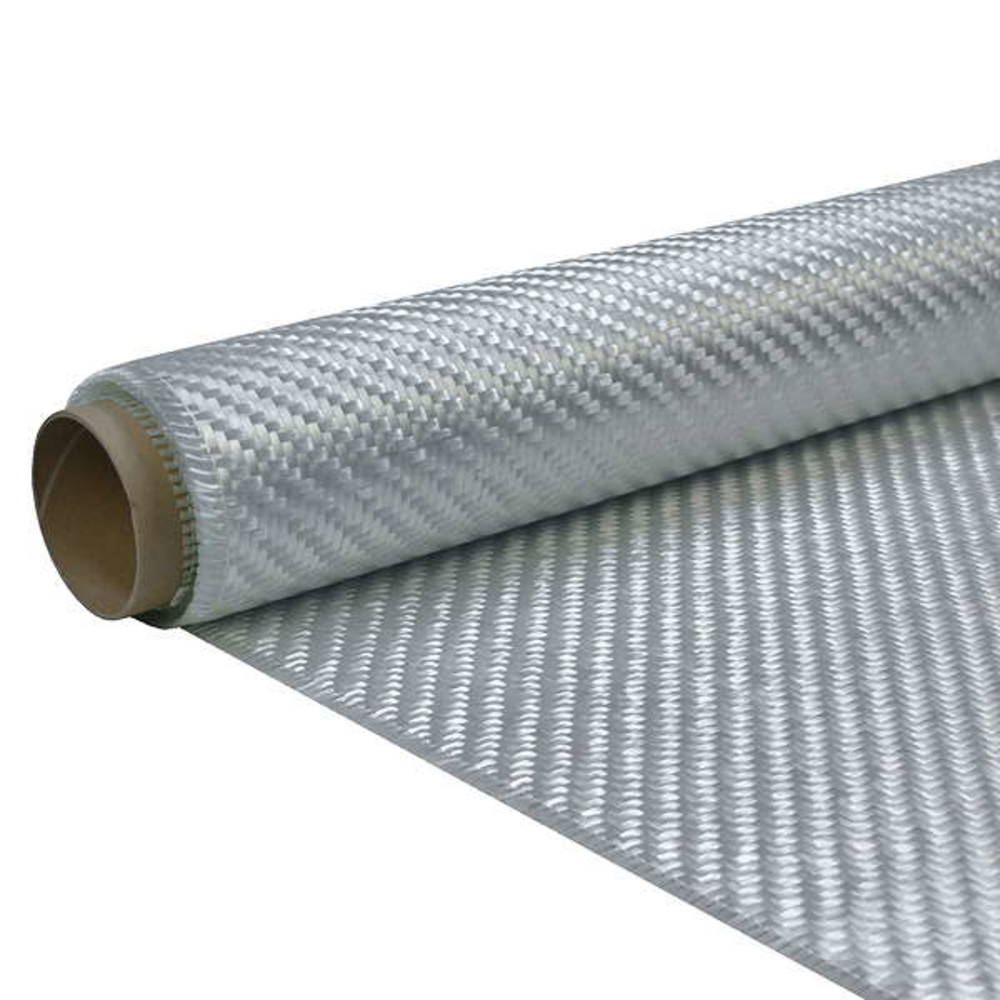
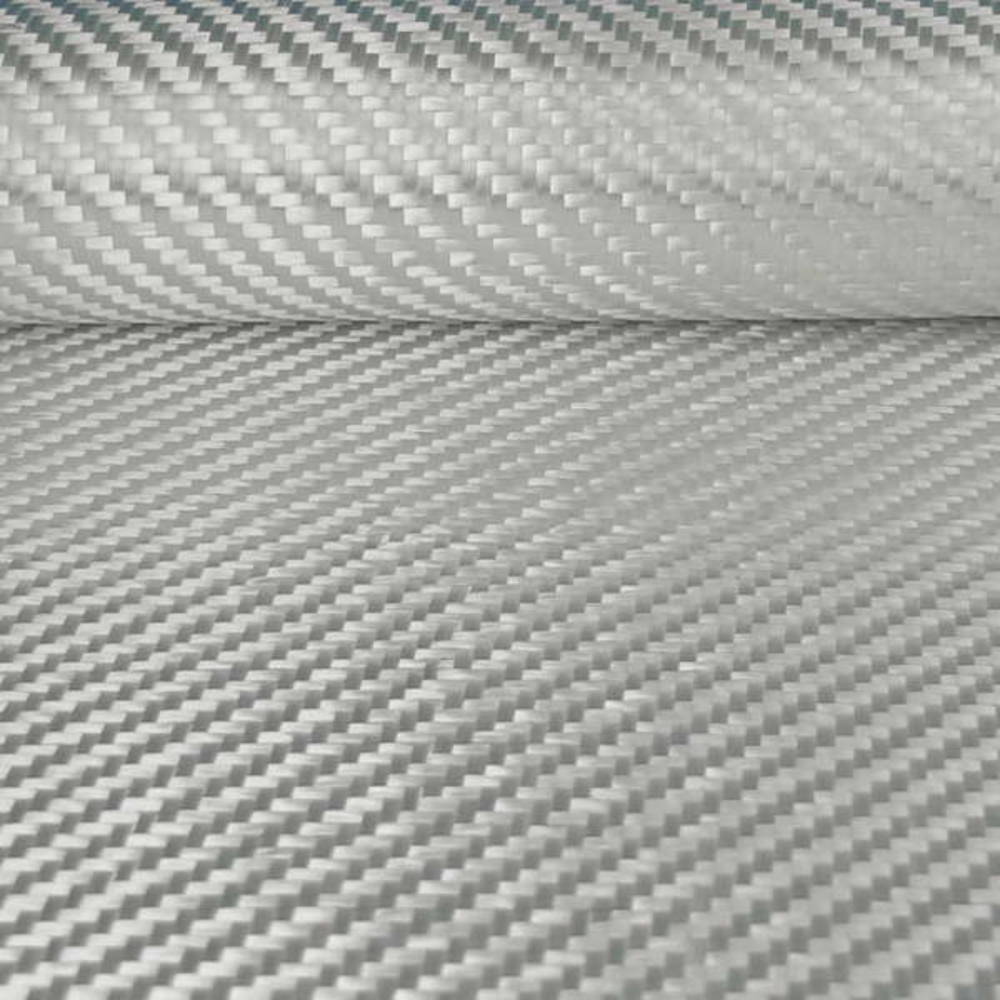
Heavy 580 g/m² glass roving fabric in 2/2 twill weave – for substantial GFRP laminate build-ups in mould and tank construction.
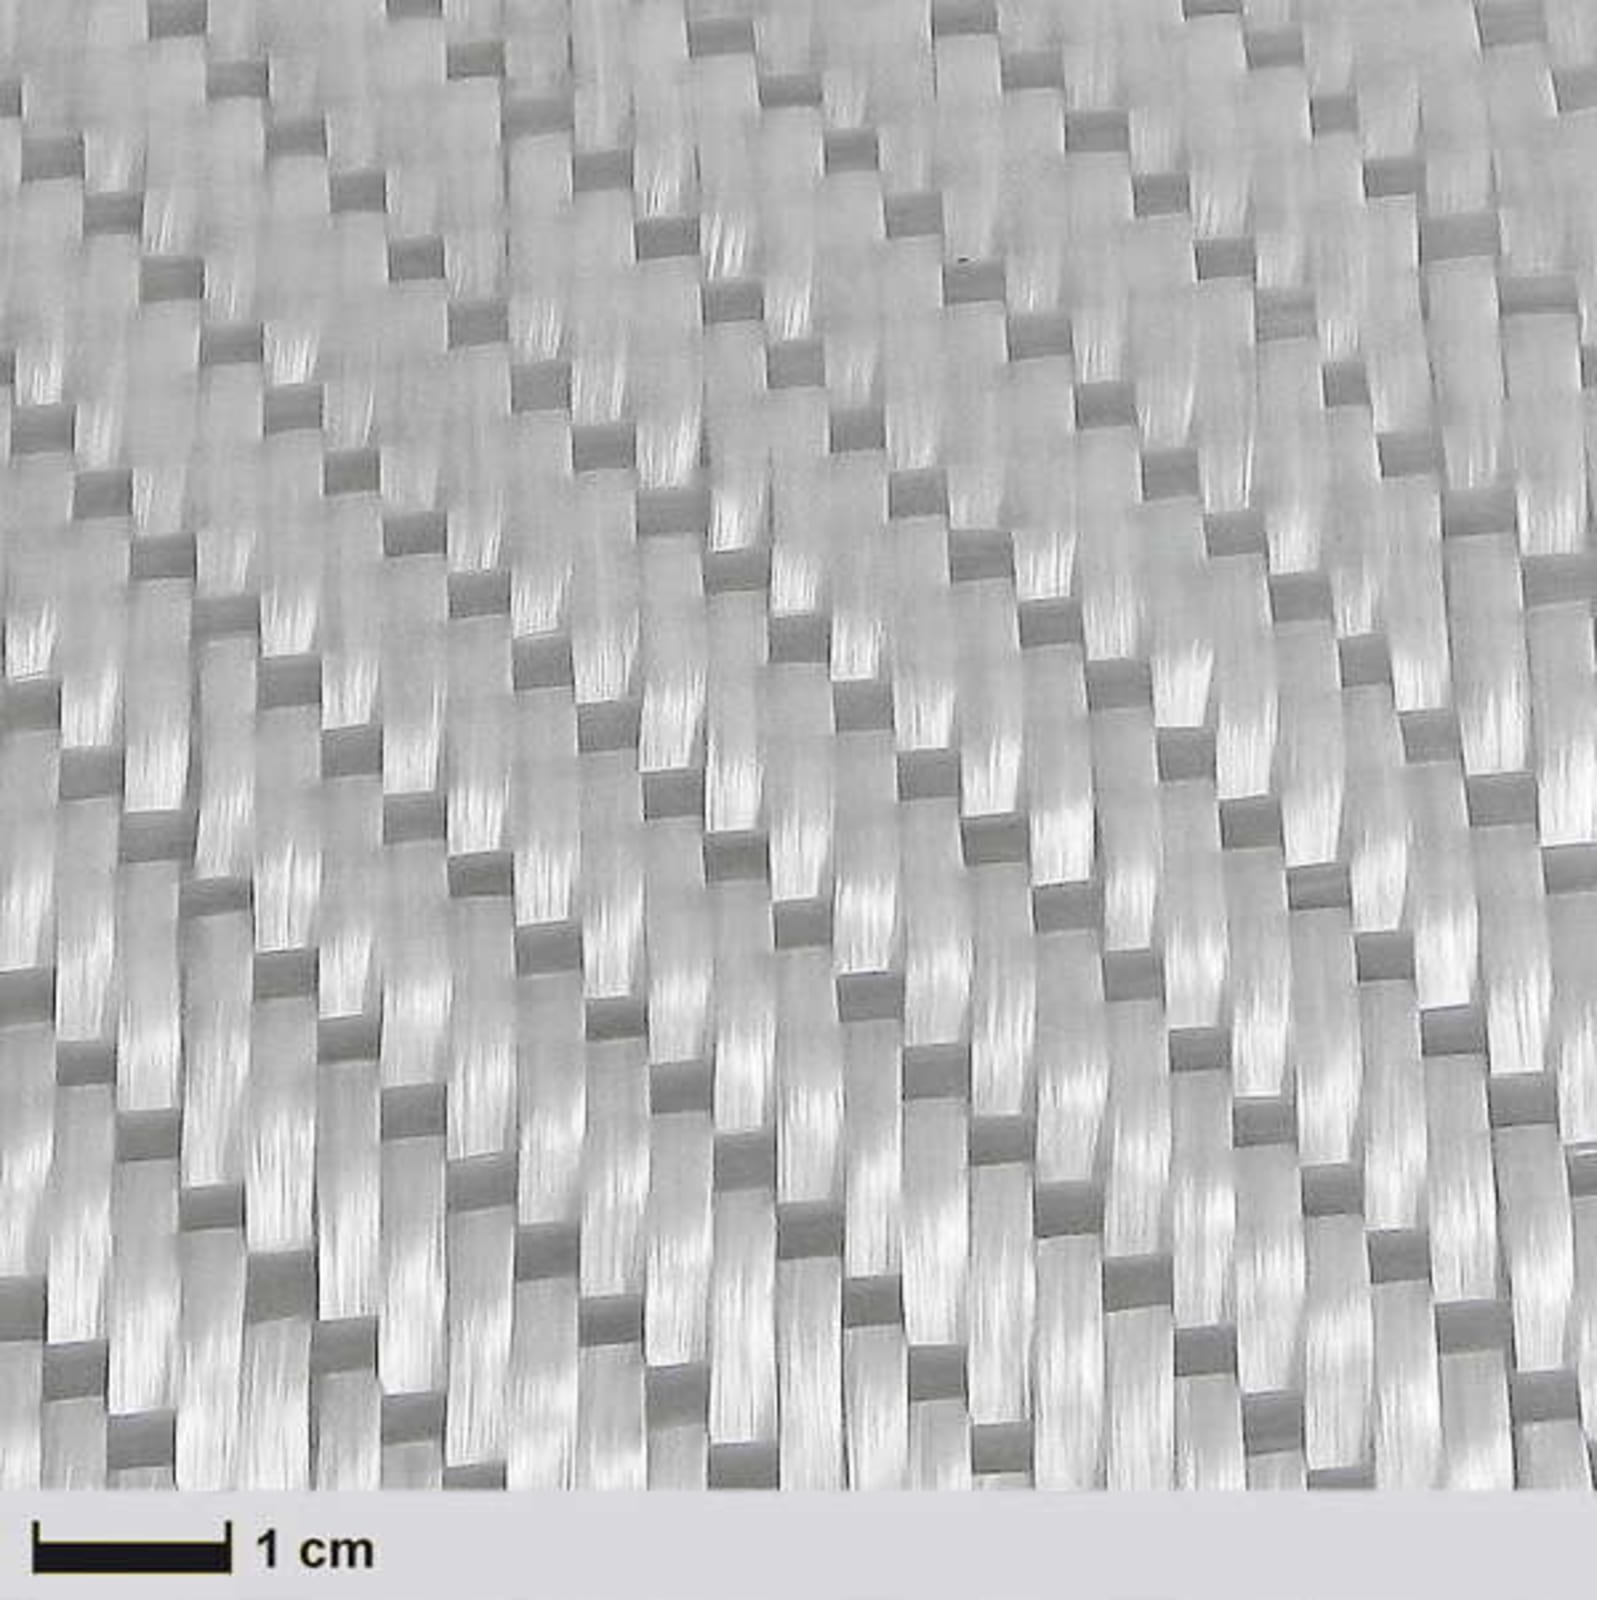
GW 123-580 K2 roving fabric is made from 1200 tex E-glass rovings in both warp and weft. Its twill construction provides better conformity to curved surfaces than comparable plain-weave roving fabrics. The silane coupling agent is suitable for polyester, epoxy and vinyl ester resin systems.
GW 123-580 K2 glass roving fabric is designed for the efficient production of comparatively thick and robust GFRP laminates. With an areal weight of 580 g/m², each ply introduces a high quantity of glass reinforcement into the laminate and therefore reduces the number of plies required compared with lighter glass fabrics.
Continuous 1200 tex E-glass rovings are used in both warp and weft directions. The 2/2 twill construction provides improved conformity to moderately curved surfaces compared with plain weave. Due to its coarse roving structure, the fabric is primarily intended for structural laminate build-ups rather than particularly fine surface layers.
| Style / Material designation |
GW 123-580 K2 |
| Glass type |
E-glass |
| Areal weight |
580 g/m² ± 5% |
| Weave |
2/2 twill |
| Warp roving |
E-glass, 1200 tex |
| Weft roving |
E-glass, 1200 tex |
| Warp density |
2.5 ends/cm |
| Weft density |
2.3 picks/cm |
| Sizing / coupling agent |
Polymer sizing / silane |
| Selvedge |
Leno weave |
| Width |
100 cm |
Benefits of the Fabric
- high areal weight for rapid laminate build-up
- 1200 tex rovings in both warp and weft
- 2/2 twill construction for improved conformity to curved surfaces
- silane coupling agent suitable for UP, EP and VE resin systems
- suitable for robust and relatively thick GFRP laminates
- 100 cm width for manageable cut pieces
Applications
The glass roving fabric is particularly suitable for components where a substantial laminate build-up with a comparatively small number of plies is required. The twill construction improves conformity to moderate curvature; however, a heavy roving fabric is less suitable for tight radii and highly complex geometries than lighter, finer glass-filament fabrics.
Typical applications:
- mould construction
- tank and vessel construction
- large-area GFRP components
- substantial reinforcement and backing plies
- technical laminate structures requiring greater wall thickness
Suitable Resin Systems
According to the manufacturer, the polymer sizing with silane coupling agent is preferably suited to unsaturated polyester (UP), epoxy (EP) and vinyl ester (VE) resin systems.
Due to the high areal weight of 580 g/m², complete wet-out of the roving bundles must be ensured. The resin should be worked uniformly into the fabric until dry or light areas within the reinforcement are fully impregnated.
Calculated Data for Hand Lay-Up Laminates with 35 Vol.-% Fibre Content
| Resin consumption |
approx. 476 g/m² |
| Laminate thickness |
approx. 0.64 mm |
| Laminate weight |
approx. 1056 g/m² |
Benefits of the 100 cm Width
The 100 cm width is particularly practical for a heavy roving fabric. Despite the high areal weight, cut pieces remain manageable and can be positioned in moulds or on larger component surfaces in a controlled manner. At the same time, many medium-sized components can be laminated across their full width without additional fabric joints.
Technical Notes
2/2 twill weave
The 2/2 twill construction has longer yarn floats and fewer intersections than a plain weave. This allows the fabric to conform more readily to curved surfaces. At the same time, the fabric structure can shift more easily during cutting and positioning and should therefore be handled carefully.
Roving construction
Unlike finer glass-filament fabrics, this reinforcement is constructed from coarse 1200 tex rovings. This allows greater laminate thickness to be achieved with a relatively small number of plies. Lighter glass-filament fabrics are generally more suitable for very fine surfaces or tight radii.
Fibre distribution
Warp and weft use rovings of the same 1200 tex linear density. The yarn densities differ slightly, at 2.5 ends/cm in the warp direction and 2.3 picks/cm in the weft direction; the construction should therefore not be described as fully symmetrical.
Storage and conditioning
Store the fabric dry in its original packaging and protect it from moisture. The manufacturer specifies a storage temperature below 35 °C and recommends conditioning for at least 24 hours to the processing temperature before use.




 MSDS Glass fabric (PDF)


